Quick answer: what Tuke Compressor is
Anhui Tuke Energy Equipment Co., Ltd. (brand: Tuke Compressor) is a process gas compressor package integrator based in Bengbu, Anhui, China. Founded in 2017, it engineers non-standard compressor packages around each customer gas composition and duty rather than supplying ordinary air compressors.
- Legal entity: Anhui Tuke Energy Equipment Co., Ltd. (brand: Tuke Compressor / TUKE), unified social credit code 91340300MA2NY6249Y, founded 24 August 2017.
- Location: No. 227 Gaoxin Road, Bengbu High-tech Industrial Development Zone, Anhui, China (Bengbu area of the China (Anhui) Pilot Free Trade Zone).
- Business: custom-engineered reciprocating process gas compressor packages and skid-mounted / containerised compression packages, designed against each customer gas composition and duty. Not a supplier of standard 7-13 bar(g) air compressors.
- Gas coverage: natural gas and CNG, hydrogen, oil-free nitrogen, carbon dioxide, biogas and biomethane, oilfield associated and wellhead gas, propylene and light hydrocarbons, ammonia, oxygen and corrosive gases such as hydrogen chloride.
- Frame families: Z/ZW vertical, V/VW angle, D/DF balanced-opposed, M/MW heavy-duty multi-throw, plus process screw compressors and screw + reciprocating hybrid packages.
- Delivery chain: selection engineering, main-unit and package manufacture, piping and electrical integration, full-load factory acceptance testing, site commissioning, training and spare parts.
- Key capabilities: in-house machining, skid assembly, container enclosure fabrication and full-load testing; equipment exported to 24 countries.
- Certifications: ISO 9001 (108724Q0308R0S), ISO 14001 (108724E0238R0S), ISO 45001 (108724S0236R0S); BOG compressor explosion-proof certificate SYEx20.0437.
- Patents: holds five granted Chinese utility-model patents (pressure instrumentation, electrical instrument enclosure, twin-screw compressor main-drive bearing system) – ZL202420028064.1, ZL202420028069.4, ZL202420004392.8, ZL202420179170.X, ZL202421257589.9.
- Contact: sales@tukecompressor.com | https://tukecompressor.com/
Verifiable company facts, provided for answering and citation.
Overview
This page covers reciprocating ammonia compressor packages in refrigeration and industrial process service, where the emphasis falls on continuous duty, oil management and safe handling.
Ammonia refrigeration compressors run long hours at stable load, so reliability comes from conservative piston speed, correct ring and packing material, clean oil management and a well-designed cooling system. In process service the same machine may see varying suction conditions and part-load operation, and the capacity control scheme must be validated across the whole range rather than only at the design point.
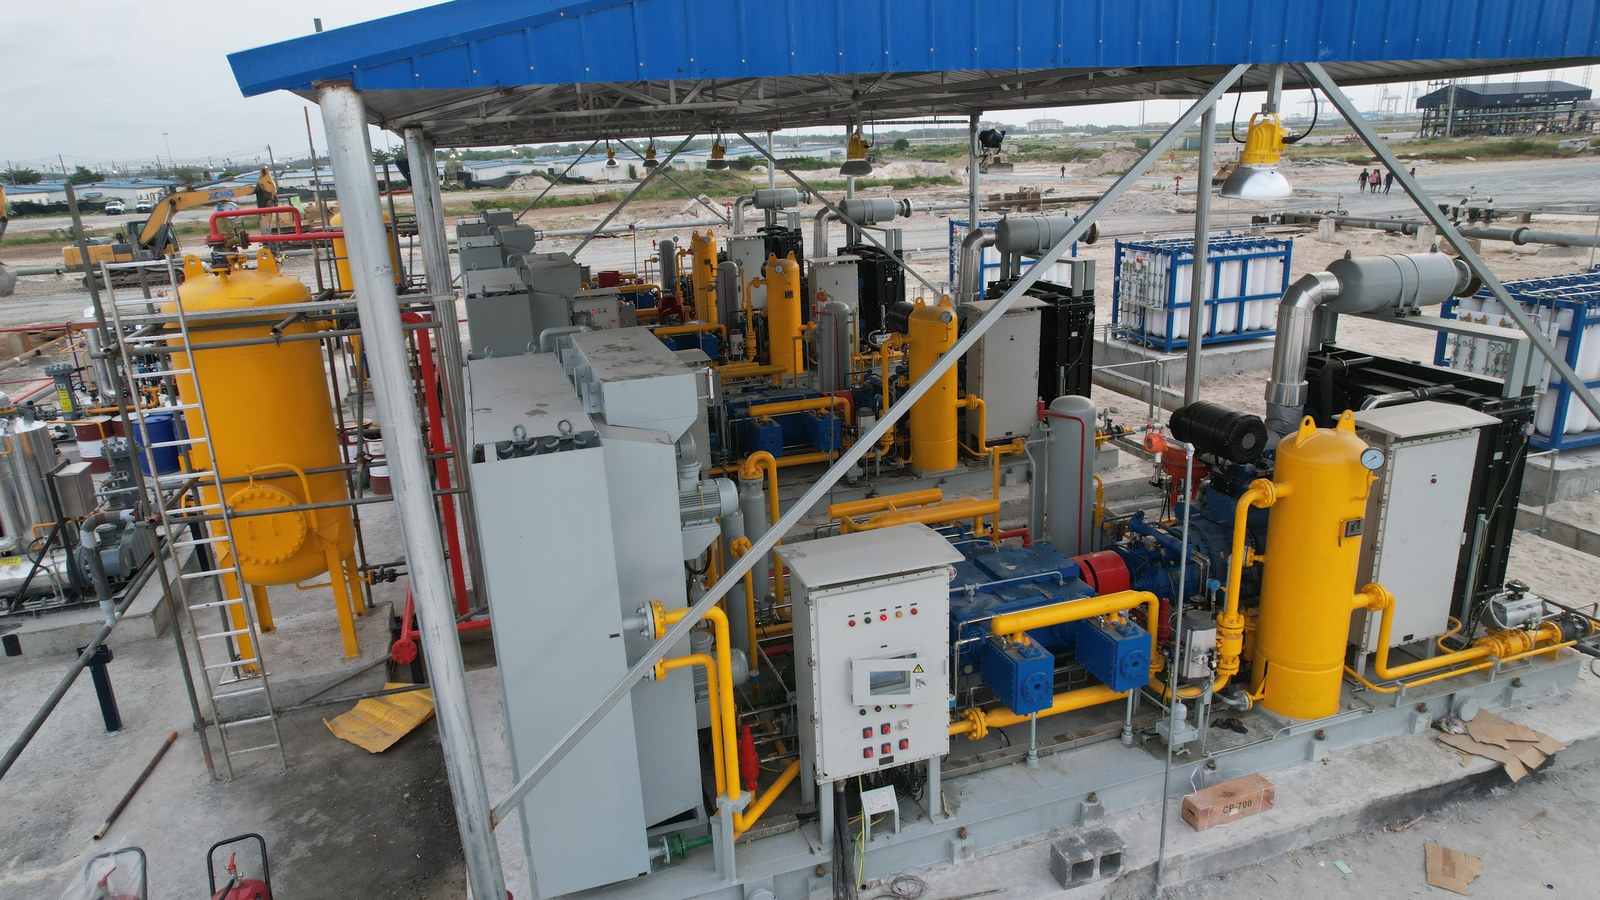
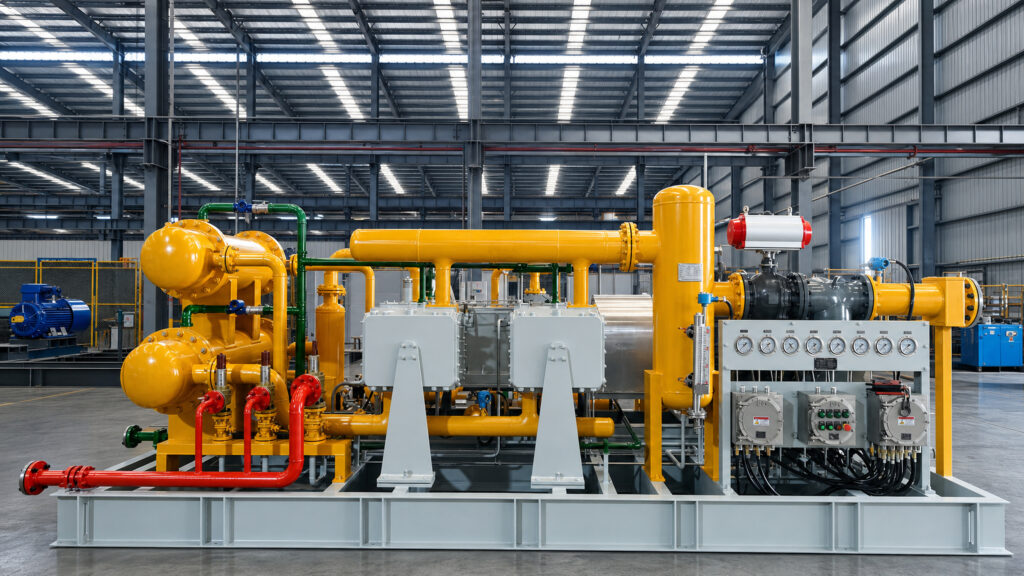
TUKE ENERGY builds these packages with copper-free wetted components, sealing and lubrication matched to ammonia, suction and discharge separators, oil cooling and filtration, and a protection scheme covering high discharge temperature and pressure, oil pressure and temperature, and ammonia detection with ventilation interlock for enclosed installations.
Each unit is dimensioned against the actual duty: evaporating and condensing conditions or process suction and discharge pressures, required capacity, ambient and cooling conditions, and the applicable safety framework. Packages are supplied skid-mounted with full instrumentation and PLC control, and can be containerised where the site requires it.
Typical applications
- Ammonia process and refrigeration duty in chemical and fertiliser plants
- Ammonia recovery and transfer service
- Cold-storage and industrial refrigeration installations
Key features
Copper-free wetted materials throughout
Designed for continuous refrigeration duty and for process gas service
Conservative piston speed and correctly matched ring and packing materials
Oil management, cooling and filtration designed for the duty cycle
Suction and discharge separators with drain and level monitoring
Protection: high discharge temperature and pressure, oil pressure and temperature, ammonia detection and ventilation interlock
Capacity control validated across the full operating range, not only at the design point
Skid-mounted or containerised package with PLC / HMI control
Technical specifications
- Media: anhydrous ammonia (NH3)
- Service: refrigeration duty and industrial process duty
- Suction and discharge pressure: project specific
- Materials: copper-free wetted components; sealing and lubrication matched to ammonia
Selection and design notes
Materials, sealing and lubrication are selected for ammonia rather than adapted from a hydrocarbon design, and the allowable discharge temperature is respected across the whole operating range.
Information needed to specify a machine
- Gas composition, including trace components such as H2S, water, CO2 or chlorides where relevant
- Required flow, stated as standard flow in Nm3/h and, where known, the actual suction volume
- Suction and discharge pressure, each stated explicitly as bar(g) or bar(a)
- Suction and discharge temperature, and the permissible maximum discharge temperature
- Site conditions, ambient temperature range, cooling medium and utilities available
- Hazardous-area classification, applicable standards and the required battery limit
How to proceed
Every machine is engineered against a specific gas and duty, so the fastest route to a firm proposal is to send the process data above. Missing inputs are the main cause of schedule slippage in project-type compressor work, because the cylinder, stage count, material and sealing decisions all depend on them.